What Causes Porous Welds? Common Shop Faults

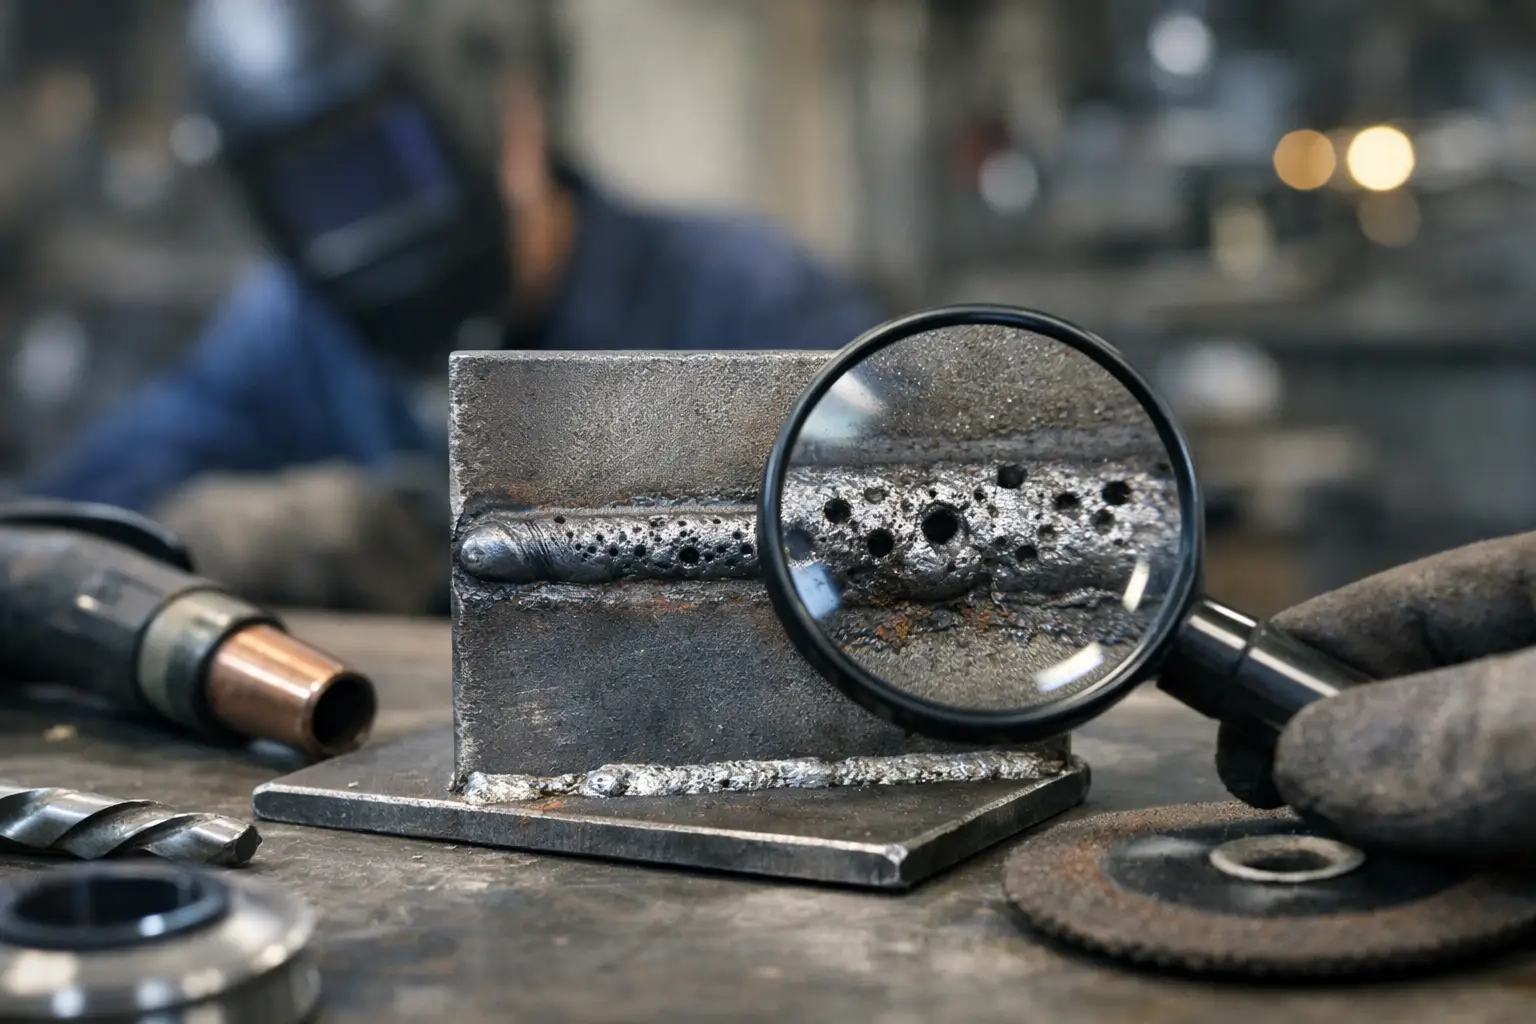
A weld can look tidy until it is cleaned, ground back or dye-checked, then the pinholes show up. If you are asking what causes porous welds, the short answer is gas getting trapped in the molten weld pool. The useful answer is finding where that gas came from before the fault turns into rejected work, rework and lost time.
Porosity is not one single problem. It can be caused by contamination in the joint, poor shielding-gas coverage, damp consumables, incorrect parameters or even a draught moving through the workshop. The shape and position of the pores often point towards the cause, but the best fix starts with a disciplined check of the whole welding set-up.
What causes porous welds in practice?
During welding, the molten pool needs protection from the surrounding atmosphere. Oxygen, nitrogen and hydrogen can dissolve into hot weld metal. As the weld cools and solidifies, those gases may come out of solution and leave cavities behind. Those cavities are porosity.
With MIG and TIG welding, poor shielding is a frequent culprit because the process relies on a stable gas envelope. With MMA welding, moisture in electrodes, poor joint preparation and arc length are common causes. Flux-cored wires bring their own considerations, particularly wire condition, polarity and the suitability of gas-shielded versus self-shielded wire for the job.
A few tiny surface pores may be cosmetic on non-critical work, but do not assume they are harmless. Porosity can reduce effective weld section, compromise fatigue performance and create leak paths in pipework, tanks and pressure-related fabrication. Where a procedure, drawing or inspection standard applies, acceptance is based on the required code, not whether the weld “looks alright”.
Contamination in the joint and on the filler
Oil, grease, paint, galvanising, moisture, cutting fluid and heavy oxide all introduce gases or prevent clean fusion. Aluminium is particularly unforgiving because its oxide layer melts at a far higher temperature than the parent metal, while surface contamination can quickly lead to hydrogen porosity. Stainless steel and mild steel may hide contamination more easily, especially on material that has been stored outside or handled with oily gloves.
Clean the joint before welding, not after the first pass goes wrong. Remove coatings well beyond the weld area, degrease with a suitable product and use clean, dedicated abrasives where material cross-contamination matters. On aluminium, use a stainless steel wire brush reserved solely for aluminium, then weld promptly rather than leaving the prepared joint exposed to workshop dirt and moisture.
Do not overlook the filler material. A MIG wire collecting dust in an open bay, TIG rods handled with contaminated gloves, or electrodes left out overnight can all put unwanted material into the pool. Store consumables dry, clean and protected. Low-hydrogen MMA electrodes need controlled storage and, where specified by the manufacturer or welding procedure, proper reconditioning in an electrode oven. A heated quiver helps keep rods in usable condition at the work area, but it does not replace correct storage of the unopened and opened packs.
Shielding gas faults: the usual MIG and TIG offender
A full-looking gas cylinder does not prove that gas is reaching the weld correctly. Check the whole route: cylinder valve, regulator, hose, connections, machine solenoid, torch lead, liner, torch neck, diffuser, contact tip and nozzle. A loose fitting or split hose can admit air without creating an obvious leak. Listen for leaks, inspect connections and use an approved leak-detection method where necessary.
Gas flow needs to be right, rather than simply high. Too little flow allows air into the weld pool. Too much flow can create turbulence and pull surrounding air into the gas shield, particularly with a narrow nozzle or in a draughty area. Flow requirements depend on process, nozzle size, torch angle, joint access and local conditions, but blindly winding the regulator up is rarely the answer.
A blocked or spattered nozzle is another regular cause. Heavy spatter disturbs gas flow and can reduce coverage just when the weld needs it most. Clean the nozzle, inspect the diffuser holes and replace damaged consumables. On MIG work, make sure the contact tip is correctly recessed or protruding for the torch set-up and that the nozzle size suits the job.
Torch technique matters too. Excessive stick-out, an over-long TIG arc, poor torch angle or travelling too quickly can move the gas shield away from the molten pool. Keep the torch stable, maintain a sensible arc length and avoid dragging the nozzle so far from the joint that coverage breaks down. When welding outside or near open roller doors, use screens or reposition the work. Even a modest draught can disrupt argon-based shielding gas.
Wrong gas, wrong wire or a compromised supply
The shielding gas must match the process and material. A mild steel MIG wire intended for argon-carbon dioxide mixes will not deliver its best results on an unsuitable gas, while stainless and aluminium each need the correct wire and shielding arrangement. Confirm the cylinder label rather than relying on its colour or where it was stored.
Gas mix mistakes often appear after a cylinder change, particularly in busy bays with several processes in use. A wrong cylinder, a crossed connection or an empty cylinder that has been run until pressure collapses can all cause sudden porosity. If the fault starts halfway through a shift with no changes to the material or technique, begin with gas supply checks.
For gas-shielded flux-cored wire, confirm that the polarity is correct and that the specified shielding gas is being used. Self-shielded flux-cored wire is designed to operate without external shielding gas, but it still needs correct polarity, settings and dry wire. Treat each wire type as its own system, not as a direct swap for solid MIG wire.
Parameters that leave the pool exposed
Poor parameters do not always cause porosity on their own, but they can make a gas or cleanliness issue much worse. An unstable arc, excessive spatter, erratic wire feed or a travel speed that outruns gas coverage can all leave the weld pool vulnerable.
On MIG, start with the wire manufacturer’s recommended range for wire diameter, material thickness and gas. Make small adjustments and watch the arc. A smooth, consistent transfer with stable wire feeding is easier to protect than a harsh, popping arc. Check drive-roll tension, liner condition and the correct groove profile for the wire. Slipping feed and bird-nesting are not just productivity problems – they can leave uneven deposits and inconsistent shielding.
On TIG, contaminated tungsten is a warning sign. If the tungsten has touched the weld pool, stop and regrind it cleanly. A contaminated electrode can destabilise the arc and carry unwanted material into the weld. Set post-flow long enough to protect the cooling tungsten and weld end; cutting gas too early can leave the final section oxidised and prone to defects.
MMA welders should keep a controlled, short arc length and use electrodes suited to the job. Long arcs allow atmospheric contamination, while damp electrodes can introduce hydrogen. If porosity appears repeatedly with a particular batch or packet of rods, check storage history and replace suspect consumables before changing every machine setting.
Read the pattern before changing everything
Porosity concentrated at the start of the weld can indicate poor pre-flow, contaminated start areas or an inconsistent gas delivery. Pores running along the bead often suggest a steady shielding or contamination issue. Porosity appearing at the end can point to poor post-flow on TIG, a broken gas shield as the torch moves away, or contamination in the crater.
Random pores across several jobs deserve a practical inspection rather than guesswork. Check the material preparation, then test gas delivery at the torch. Inspect the nozzle and diffuser, confirm the gas type and flow, look for draughts, and review torch angle and stick-out. Change one variable at a time where possible. Altering gas flow, voltage, wire speed and technique together may hide the real cause until it comes back on the next job.
For production work, keep a record of wire batch, gas type, settings and any corrective action. This is especially useful where several welders share equipment or where a job is subject to visual inspection, NDT or customer traceability. It also makes it easier to identify whether the fault follows a machine, torch, consumable batch or operator technique.
When the problem needs a closer look
If you have cleaned the material, changed the consumables, confirmed gas flow and still see porosity, inspect the torch and machine properly. A worn solenoid, damaged torch cable, blocked gas passage or inaccurate flowmeter can create faults that are difficult to spot from the outside. At that point, a service check is cheaper than repeatedly repairing finished fabrication.
Linc-Weld can help workshops narrow down equipment and consumable issues, from selecting the correct gas-shielded set-up to arranging machine repair and calibration support. The fastest route to cleaner welds is rarely a bigger regulator setting. It is a clean joint, dry consumables, sound gas coverage and a set-up that is checked before the job reaches inspection.