Plasma Cutter Air Supply Guide for Clean Cuts

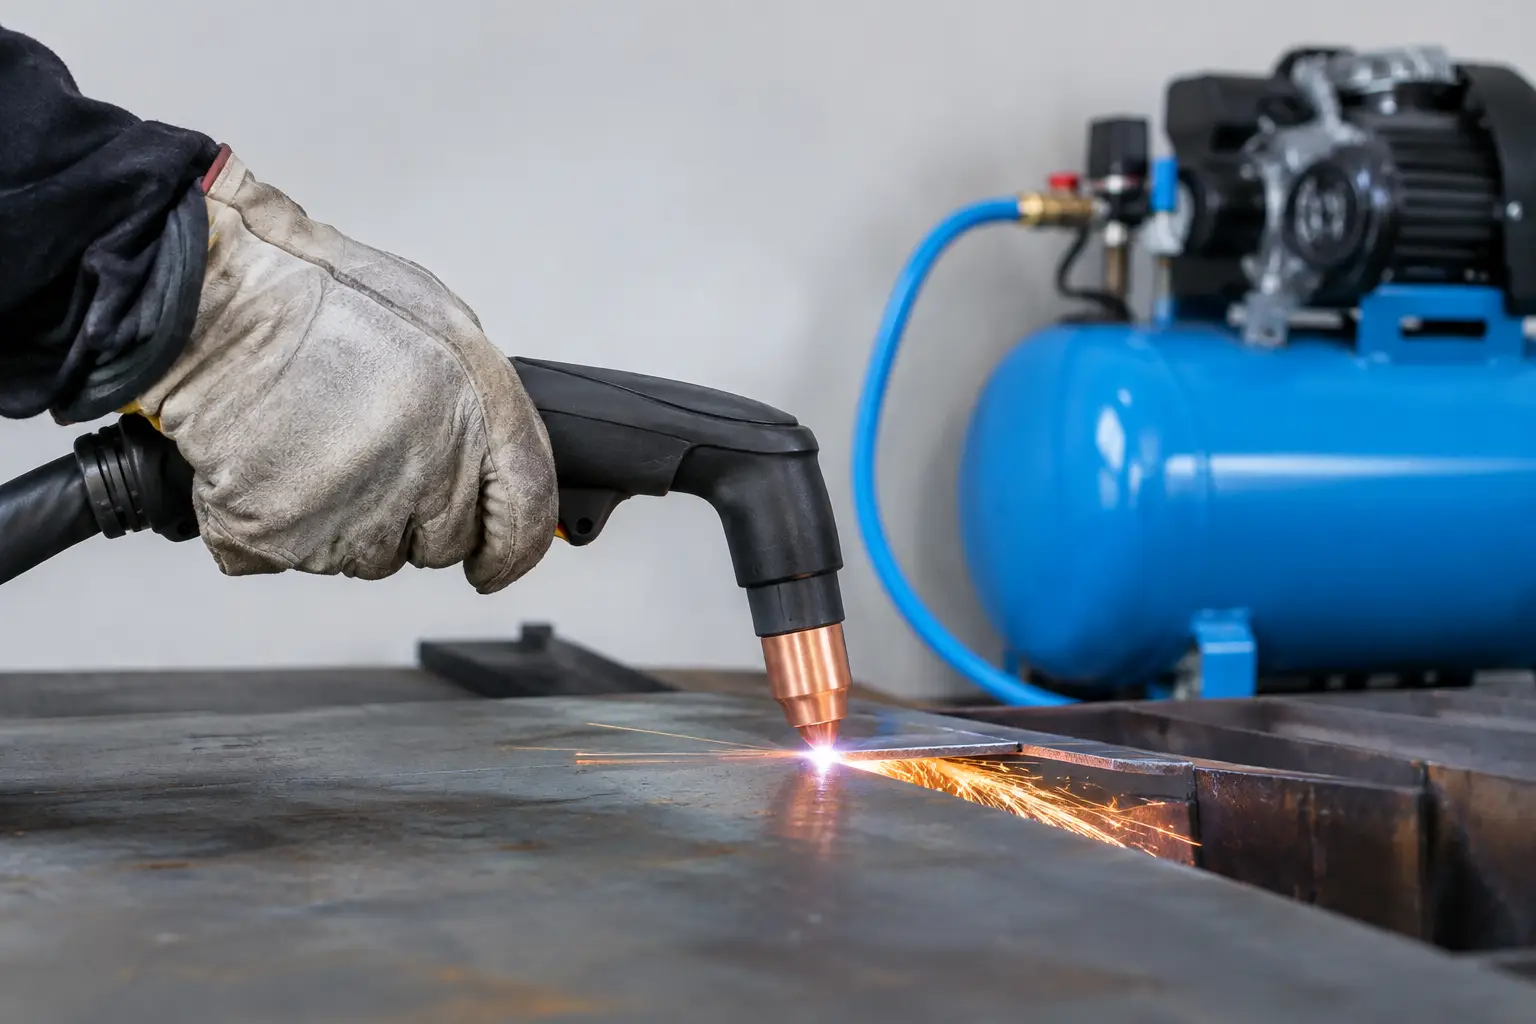
A plasma cutter can have the right amperage, the right torch and a fresh set of consumables, then still produce a rough, slow cut because the air supply is not up to the job. Weak airflow, pressure drop and moisture are among the most common causes of poor cut quality and short electrode and nozzle life. This plasma cutter air supply guide covers what a professional workshop needs to check before blaming the machine.
Start With the Plasma Cutter Specification
Every plasma cutter has a stated air requirement, normally shown as litres per minute (L/min), cubic feet per minute (CFM) or both, at a specified operating pressure. Check the machine manual or data plate rather than relying on a general compressor rule of thumb. A compact inverter plasma may need around 100 to 170 L/min, while a higher-output machine for regular fabrication can require 200 L/min or more.
The figure that matters is the air consumption at the torch while cutting. Do not confuse it with the compressor’s maximum pressure or its advertised displacement. A compressor may claim a high litres-per-minute figure but deliver considerably less free air delivery (FAD) once it is operating at working pressure. FAD is the useful number for comparing compressors against a plasma cutter’s demand.
Pressure matters too. Many air plasma systems operate around 4.5 to 6 bar, but requirements vary by model. Setting the regulator above the stated pressure does not compensate for poor air volume. It can create unnecessary turbulence, waste air and make the torch harder to set correctly. Start with the manufacturer’s recommended cutting pressure, then check the reading while air is actually flowing through the torch.
Size the Compressor for Real Cutting Time
A compressor that can just meet the cutter’s stated demand may be acceptable for occasional repairs. It is rarely the best choice for a fabrication bay where the operator is making repeated cuts all day. Plasma cutting is a continuous air-demand process, particularly on long cuts or when gouging.
As a practical working margin, choose a compressor with FAD at least 25 to 50 per cent above the plasma cutter’s stated consumption. If the cutter requires 180 L/min at 5 bar, look for at least 225 L/min FAD, and preferably closer to 270 L/min where cutting is frequent. That reserve helps the compressor recover, reduces pressure sag and prevents it running flat out for every job.
The right capacity depends on the workload:
- For light maintenance work and short, occasional cuts, a quality direct-drive or small belt-driven unit may be suitable if its FAD meets the requirement.
- For regular fabrication, a belt-driven compressor with a larger receiver generally gives more stable output and better serviceability.
- For production cutting, shared airline systems or multiple air users, a properly sized industrial compressor and air treatment setup is the sensible investment.
- For site work, match the plasma cutter to a generator-driven compressor only after checking delivered airflow and pressure under load, not its headline rating.
Receiver size is useful, but it is not a substitute for compressor output. A large tank gives a short reserve and smooths demand. Once the receiver pressure falls, however, the compressor still needs enough FAD to support the torch. If pressure falls midway through a cut, the answer is normally more available air capacity, not simply a bigger receiver.
Watch for Pressure Drop in the Airline
A regulator set at 5.5 bar beside the compressor tells you very little if the torch receives 4 bar after passing through 20 metres of narrow hose, quick couplers and water traps. Pressure drop is a workshop problem, not just a compressor problem.
Keep the route from compressor to cutter sensible. Use adequately sized airline, good-quality fittings and as few restrictions as practical. Avoid running a high-demand plasma cutter through a long, small-bore coiled hose intended for tyre inflation. Inspect couplers for damage and make sure the fittings are fully matched. A partly connected quick-release coupling can restrict airflow enough to affect cutting while still appearing to work.
The simplest test is to watch the pressure at the cutter with the torch triggered. If it falls below the machine’s required operating pressure, investigate the supply before changing torch parts or machine settings.
Dry, Clean Air Protects Consumables
Compressed air naturally carries water vapour. As it cools in the receiver, pipework and hose, that vapour condenses into liquid water. Add compressor oil carryover, rust from old pipework and workshop dust, and the air reaching the torch can become a costly mixture.
Moisture causes unstable arcs, excessive dross, poor edge finish and rapid consumable wear. Oil contamination can be even more damaging. It leaves deposits within the torch and interferes with the plasma process, often showing up as erratic starting or a nozzle that burns through far earlier than expected.
Drain the compressor receiver regularly. In a busy workshop, make it part of the daily routine, especially during cold or damp weather. Automatic drains are worthwhile where the compressor runs frequently, but they still need checking. A blocked automatic drain is no better than no drain at all.
For dependable plasma cutting, fit air treatment close to the machine. A basic water separator helps, but it may not remove enough moisture when the air is hot or the ambient conditions are humid. A sensible setup uses a particulate filter and water separator, followed by a coalescing filter where oil carryover is a concern. For regular professional work, a refrigerated dryer provides a far more consistent supply of dry air than relying on a bowl filter alone.
Desiccant dryers can achieve very dry air, but their media needs replacing or regenerating. They are often best used as a final polishing stage for sensitive applications, rather than as the only treatment on a heavily used airline. The right setup depends on cutting hours, compressor type and how clean the existing air system is.
Keep the Plasma Line Separate Where Possible
Do not assume a workshop ring main is automatically suitable for plasma cutting. Lines that feed air tools may have lubricators fitted, and lubricated air must not feed a plasma cutter. Take the plasma branch before any lubricator, or run a dedicated clean-air line.
It is also good practice to place the final filter and regulator near the cutter rather than at the far end of the workshop. That reduces the chance of water condensing again in a long hose after it has been filtered. Clear filter bowls make inspection quick, but replace elements to schedule rather than waiting for obvious failure.
Set Pressure With Air Flowing
Most plasma cutters have either a built-in regulator, a pressure gauge or an air-test function. Use it. Set the pressure with the torch air flowing, because static pressure can look correct and then collapse once cutting begins.
If your machine has an air test mode, run it after connecting the supply and after changing filters or hoses. Listen for leaks around the torch connection, regulator and couplers. A small leak can force a compressor to cycle more often; a major leak can prevent the cutter reaching its required pressure altogether.
Do not use the plasma cutter’s regulator to correct a badly configured compressor. The compressor should provide stable pressure above the cutter’s requirement, allowing the machine regulator to reduce it accurately. If the supply pressure is constantly on the edge, the regulator has nothing to work with.
Signs Your Air Supply Is Letting You Down
Poor air quality and inadequate volume often look like a torch problem. Before replacing consumables, check the air system when you see rough cut faces, heavy dross, repeated arc-outs, difficulty piercing, inconsistent kerf width or unusually fast nozzle and electrode wear.
A good diagnostic routine starts at the compressor. Confirm the receiver is drained, check the FAD rating against the cutter requirement, inspect filters and then test dynamic pressure at the machine. Next, examine the hose and couplers. Only then move on to torch consumables, work lead connection, earth clamp condition and cutting technique.
Consumables should wear gradually and evenly. If a nozzle or electrode fails after only a short period, contamination is a likely cause. Replacing parts without fixing wet or oily air simply repeats the expense.
A Better Air Setup Pays Back Quickly
Plasma cutting air is not an afterthought. It is part of the cutting system, just like the torch, work clamp and consumables. A correctly sized compressor, stable pressure and properly treated air give cleaner cuts, fewer failed starts and lower consumable spend.
For workshops buying a new plasma cutter or upgrading an existing bay, specify the air supply at the same time as the machine. Linc-Weld can help match cutting equipment, compressors, air treatment and consumables to the work being done, so the first cut is not held back by the air behind it. Start by checking the cutter manual, then test pressure at the machine under flow – that five-minute check can save a full day of poor cutting.